Our Story
Built on passion, precision, and a commitment to quality — Heartbeat Freeze Drying is your trusted partner in food preservation.
A Passion for Preservation
Heartbeat Freeze Drying was founded with a simple mission: to provide businesses with access to professional, high-quality freeze drying services without the massive capital investment of owning their own equipment.
What started as a small operation has grown into a trusted partner for food brands, preparedness companies, and specialty producers across the country. Our state-of-the-art facility is equipped with commercial-grade freeze dryers capable of processing thousands of pounds per cycle.
Every product that leaves our facility carries the Heartbeat promise — precision-dried, quality-tested, and packaged to perfection.
Mission & Values
Our mission is to make commercial-grade freeze drying accessible, reliable, and affordable for businesses of all sizes.
Passion for Preservation
We are driven by a genuine passion for freeze drying and the incredible benefits it brings to food preservation.
Precision & Excellence
Every batch is processed with meticulous attention to detail, ensuring consistent, superior results.
Customer Partnership
We work closely with our clients to understand their needs and deliver tailored solutions that drive their success.
Safety First
Food safety is non-negotiable. We maintain the highest standards in sanitation, handling, and compliance.
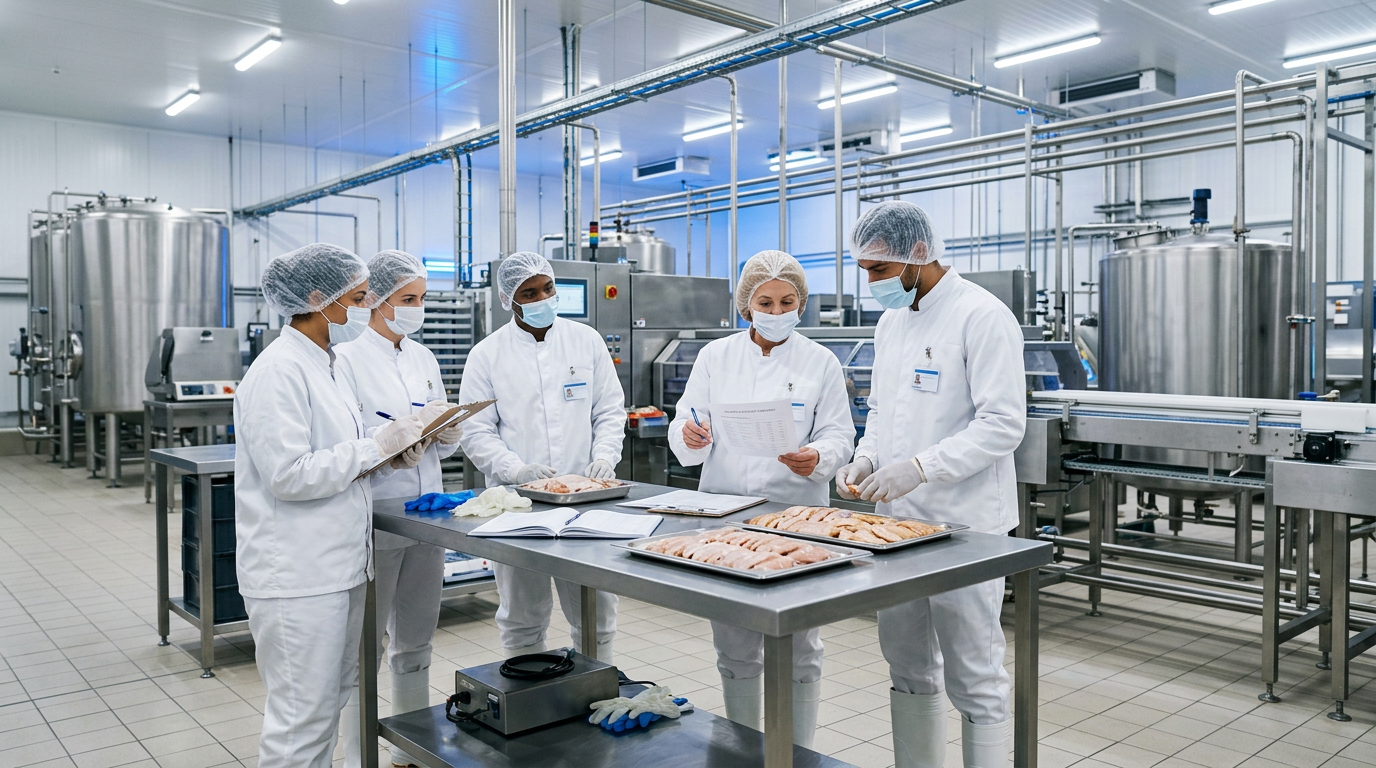
Quality & Safety Standards
We hold ourselves to the highest standards in food safety, quality assurance, and regulatory compliance.
FDA Compliant Facility
Our processing facility meets and exceeds FDA food safety regulations, with regular inspections and updated protocols.
HACCP Certified
We follow Hazard Analysis Critical Control Point principles to identify, evaluate, and control food safety hazards.
Batch Testing
Every production batch undergoes moisture analysis, water activity testing, and visual quality inspection before release.
SOPs & Documentation
Comprehensive standard operating procedures and full traceability from raw ingredient to finished product.
Third-Party Lab Testing
Independent lab verification ensures our products meet all safety and nutritional standards.
Allergen Management
Strict allergen control protocols and dedicated processing areas to prevent cross-contamination.
Meet the Experts
Our dedicated team brings years of experience in food science, processing, and quality assurance.
John Smith
Founder & CEO
Sarah Johnson
Operations Director
Mike Chen
Quality Assurance Manager
Emily Davis
Production Lead